This guide explains Colbate—how it is used, how suppliers typically structure sourcing, and what quality checks matter. Colbate is commonly discussed within industrial supply chains as a material or component reference, where performance depends on spec compliance, traceability, and handling. The article offers objective guidance for procurement decisions and practical due diligence.
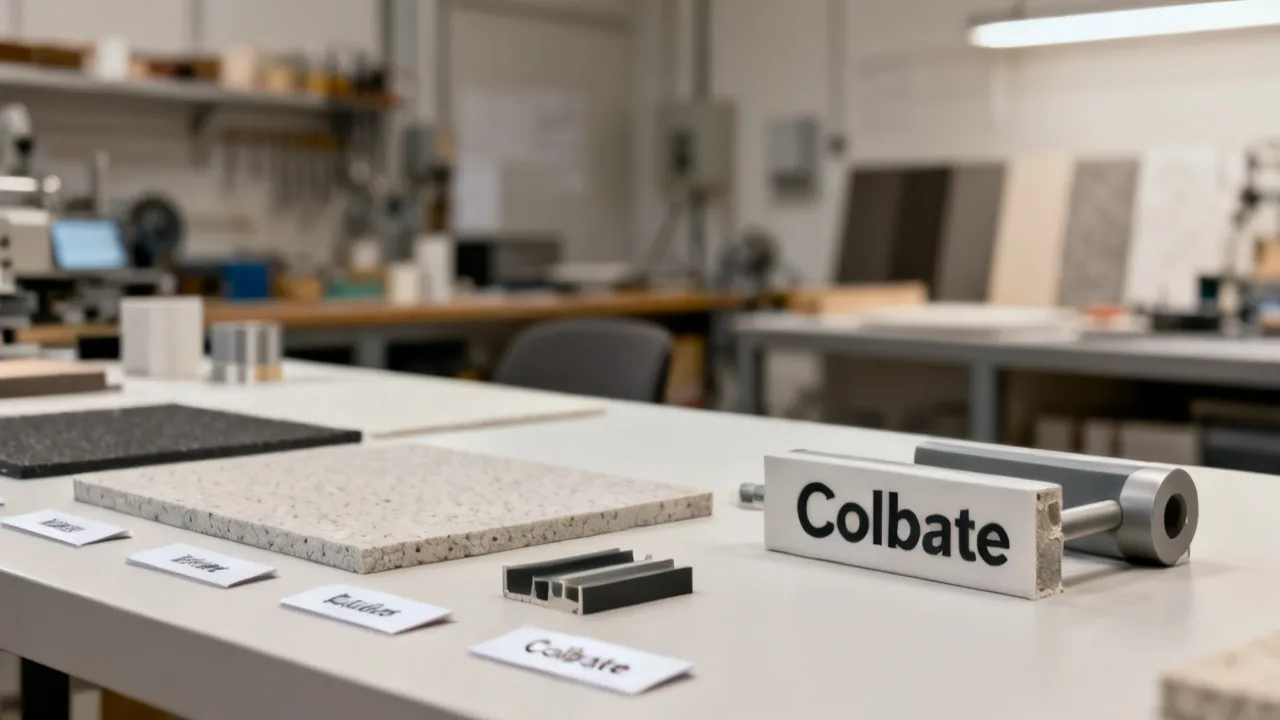
When you evaluate Colbate for industrial use, the very important decisions happen before purchase: confirming specifications, verifying supplier capability, and setting practical acceptance conditions. In very supply-chain contexts, Colbate-related procurement is less about a single “top” vendor and more about aligning technical requirements with consistent manufacturing, documentation, and handling practices.
In this article, I’ll present a professional, objective view of what “Colbate” typically implies in sourcing discussions, how experts approach qualification, and how to compare supply options without relying on marketing claims. You’ll also find a structured supplement section (comparison table, sources, step-by-step guide, and conditions) and a set of frequently asked questions.
The term Colbate appears across industrial purchasing workflows as a product/material/component reference. In practice, buyers treat such terms as identifiers that must be validated against formal technical documentation—such as a specification sheet, an agreed standard, or a declared material constitution and tolerances.
Because names in industrial sourcing sometimes vary by region, distributor, or historical cataloging, a prudent approach is to validate Colbate by:
A common misconception in purchasing is thinking that product names alone “encode” the details needed for risk control. In reality, the name is the starting point. The due diligence work is about making sure the delivered material is the same one you think you’re buying—right grade, right measurement basis, right tolerance class, right traceability mechanism, and the right recommended use envelope.
In many procurement teams, “Colbate” may be used as shorthand in an email thread or quote request. Yet when quality leadership (or regulatory affairs) gets involved, the conversation shifts quickly from “we supply Colbate” to “show us what you mean by Colbate,” including the underlying technical specification and the evidence used to claim compliance.
In many industrial categories, a supplier may describe Colbate using broadly similar language, yet the real differences show up in the fine print: test methods, measurement uncertainty, allowable deviations, and the conditions under which those tests were performed.
From an industry expert’s perspective, procurement risk usually concentrates in four areas:
Accordingly, due diligence often begins by requesting the right documents and confirming the test framework used to generate them. This is where procurement and quality assurance (QA) collaborate: procurement brings commercial context (availability, cost, lead time), while QA brings evidence standards (what the tests actually mean, what they can’t prove, and how to check the material on receipt).
Experts typically also consider the “confidence level” of any documents provided. A certificate of conformity might be legally useful, but it may not provide enough information to confirm suitability for your specific application risk. For example, two suppliers might both deliver a certificate showing “pass,” but one supplier might specify a more rigorous method, tighter tolerance bounds, or more robust sampling. Those differences can strongly influence your incoming inspection effort and your downstream failure risk.
Buyers usually compare suppliers along measurable criteria. Even if two suppliers both say they provide Colbate, “same name” does not always mean “same specification.” A careful evaluation therefore emphasizes:
Price is important, but in many industrial procurement programs the safest approach is to treat pricing as a variable that must be justified by compliance evidence. When performance failures are costly, the “low price per unit” option can become the very expensive option overall.
This “total cost” thinking often includes hidden costs such as:
To avoid these traps, experienced buyers build a structured “quote normalization” process. They do not compare quotes only by unit price; they compare quotes by what exactly is included (documentation package, test reports, traceability level, packaging protections, inspection assumptions) and how much operational friction each quote likely introduces.
Because the prompt did not include specific numeric pricing, I will avoid inventing cost figures. Instead, an objective framework helps you evaluate Colbate quotes from multiple parties:
In procurement practice, a quote that appears higher can still be economical if it reduces testing friction, shortens lead time, or improves delivery reliability—especially for projects with tight schedules.
To make this work in the real world, many organizations create a “commercial + quality scorecard.” Even if the scorecard weights are not perfect, they help prevent the common error of selecting a supplier that looks cheap on paper but is expensive in execution.
A practical way to apply this is to ask for a clear definition of deliverables in each quote, such as:
When those questions are answered clearly, price comparisons become more meaningful. Otherwise, purchasing is essentially comparing incomplete stories.
An expert view of supplier qualification centers on repeatability and verifiability. For Colbate, a capable supplier typically demonstrates:
If you encounter vague descriptions, missing test methods, or unclear lot traceability, the risk is not just “paperwork.” Those gaps can translate into operational uncertainty once Colbate enters production workflows.
It’s also important to understand that supplier capability is multi-dimensional. A supplier can have strong technical competence but weak logistics reliability, or strong documentation but limited ability to supply consistent volumes. In due diligence, teams often separate these capabilities so that they can be addressed through contractual conditions or qualification steps.
For example, if a supplier’s documentation is good but their lead times are inconsistent, you might:
Conversely, if lead times are good but documentation and traceability are weak, you might:
In other words, supplier capability must be translated into risk controls that your organization can execute.
Even when Colbate meets specifications on paper, real-world performance depends on how it is handled, stored, and integrated into your process. Industry teams commonly consider:
Operational teams typically want a short, actionable handling note—because it reduces variability and prevents avoidable failures during batch acceptance.
From a due diligence standpoint, it’s useful to ask: if something goes wrong, will you be able to identify whether the cause was the material itself, the handling, or the processing? Strong procurement documentation helps answer this by enabling “paper-to-physical” linkage. Handling guidance, in turn, tells you whether you should expect certain sensitivities (for example, moisture uptake risk, storage duration limitations, or contamination concerns).
Many organizations also integrate handling requirements into warehouse procedures. That may include:
While these details might appear “operational” rather than “procurement,” they are tightly linked. If procurement orders Colbate with incomplete handling requirements, the warehouse may apply generic practices that increase variability. Therefore, due diligence should treat handling guidance as a required deliverable.
In expert procurement workflows, acceptance is defined before shipment. For Colbate, buyers commonly establish an incoming inspection plan that includes:
Crucially, acceptance criteria should be tied to your application risk. If your process is sensitive to a particular parameter, then the inspection plan should focus on that parameter rather than performing generic checks.
Acceptance testing plans can differ depending on whether Colbate is used as a raw material, an additive, a component in an assembly, or a critical feed into a chemical or mechanical process. In many cases, the deciding factor is whether variation in a Colbate property will directly impact performance or whether it is likely to be compensated downstream.
For example, if Colbate is used in a step where trace contamination or property drift will lead to immediate failure, then incoming acceptance may require tighter sampling and more direct parameter checks. If, however, your downstream process can tolerate some variation (with adjustments or corrections), then a less intensive incoming inspection might be acceptable—provided that the supplier is well-qualified and stable.
A thorough acceptance strategy often includes:
Where appropriate, organizations also define the “relationship” between supplier tests and buyer tests. Instead of assuming that supplier tests automatically guarantee acceptance, buyers align methods and measurement definitions. This prevents mismatches where supplier test definitions differ subtly from what your QA team measures.
For industrial buyers, compliance is not only about legal requirements; it is also about assurance that quality is controlled over time. With Colbate-related purchases, procurement teams often ask for:
Where traceability is critical, experts commonly coordinate a “paper-to-physical” verification: ensuring that batch numbers, identity marks, and received units align with the paperwork.
Traceability is a quality multiplier. It reduces uncertainty during investigations and makes corrective action more effective. Without traceability, a nonconforming lot becomes difficult to contain, and the organization may have to quarantine more material than necessary—leading to scrap, schedule impact, or additional costs.
A well-designed traceability system typically includes:
Procurement due diligence should also cover data quality. If the supplier uses a lot ID format that is ambiguous (for example, unclear date codes or inconsistent character lengths), it can cause receiving errors. In practice, those errors are avoidable when procurement requires a clear labeling and documentation standard.
Compliance also tends to include supplier responsiveness obligations. For example, if a supplier identifies that a specific lot did not meet internal controls, you need a contractual pathway for notification and remediation. Due diligence includes assessing whether the supplier has a mature corrective action process and whether they are willing to collaborate during investigations.
| Evaluation axis | What to compare | Why it matters for Colbate | Evidence to ask for |
|---|---|---|---|
| Specification match | Declared grade, tolerances, and performance parameters | Prevents mismatches that can cause yield loss | Specification sheet, agreed acceptance criteria |
| Test evidence | Test methods and results by batch/lot | Supports reliable incoming inspection | Test reports referencing methods, sampling plan details |
| Traceability | Batch numbering and document alignment | Enables investigation if issues arise later | Certificates of conformity tied to lot/batch IDs |
| Supplier quality system | Operational controls and corrective action capability | Reduces good inconsistency risk | Quality framework details, audit summaries (if available) |
| Logistics and handling | Packaging method and storage guidance | Protects integrity during transport and storage | Handling instructions, packaging description |
| Total cost realism | Landed cost plus inspection and risk costs | Prevents “cheap quote” from turning costly | Clear quote scope, shipping terms, inspection assumptions |
Note: This article intentionally avoids unverified or potentially exaggerated performance claims. Where specific numeric benchmarks are required for your use case, the top practice is to rely on your application-specific test plans and supplier-provided verified documentation.
Qualification is not merely “receiving one good shipment.” It is a controlled pathway that reduces the likelihood that your organization becomes the first customer to discover an unrecognized variation in Colbate performance or properties. A good qualification trial also clarifies your own internal process: it tests how your organization handles Colbate from receipt to consumption, which is essential because operational deviations can mimic material nonconformance.
To further improve qualification quality, some organizations perform parallel checks:
This “two-sided validation” (supplier evidence + buyer operational confirmation) is often more reliable than relying solely on supplier documentation.
To reduce procurement risk with Colbate, organizations commonly require the following conditions:
Beyond the checklist, experienced procurement teams often add a few “operational safeguards” into purchase agreements:
Those additional terms help ensure that the quality system is not only present on paper but active when something goes wrong.
To make the due diligence process practical, procurement often uses a supplier questionnaire aligned to the same four risk areas discussed earlier: specification ambiguity, insufficient evidence, handling constraints, and lot inconsistency. Below is a set of questions that experienced teams frequently include during qualification for materials like Colbate.
These questions can feel detailed, but they save time later. They convert quality risk from a vague concern (“We hope it works”) into a measurable and testable structure.
When designing an acceptance plan, the goal is not to “test everything.” The goal is to test the right things with the right frequency at the right decision points—while minimizing operational burden and schedule delays.
A practical plan often uses a layered approach:
For Layer 1, buyers typically confirm that the lot number on the certificate matches the lot number on packaging and receiving records. They also verify that the certificate includes the key properties required by the specification and by your application risk profile.
For Layer 2, the question is how many units or how much material should be tested. Sampling frequency might depend on:
For Layer 3, application verification can mean running a controlled process step with the delivered Colbate and verifying the resulting output meets your internal acceptance criteria. This is especially useful when lab tests alone do not predict operational performance because of processing dependencies.
Even if application verification is not required every shipment, it is useful for:
When a delivered Colbate lot fails acceptance criteria, the next steps matter as much as the failure itself. A disciplined response prevents the organization from repeating the same issue, and it prevents supplier/customer blame loops from consuming time.
Experts typically handle nonconformities using a structured logic:
Importantly, the buyer should also consider whether the nonconformity could be due to receiving/handling issues. If storage conditions or warehouse procedures differ from the supplier’s recommended envelope, a lot might fail tests even if the supplier produced it correctly. This is why the due diligence process includes handling guidance and internal alignment.
One of the most common procurement risks in materials like Colbate is not outright noncompliance, but “silent change.” A supplier might adjust raw inputs, tooling, measurement standards, or processing conditions and continue delivering under the same product name.
To mitigate this, procurement teams establish:
In practice, change control also includes measurement method control. If a supplier changes their internal test equipment or method, your organization may need to interpret results differently. Procurement should request clarity on how test method changes affect comparability over time.
Quality due diligence is not only about test results. It also includes reliability of supply and continuity of manufacturing processes. Even a well-qualified supplier can become risky if they:
To address this, procurement can require:
These requirements keep quality consistent even when commercial pressures increase.
Colbate procurement succeeds when internal teams act as one system. If procurement negotiates terms that QA cannot execute (for example, if documentation is missing but procurement accepts it anyway), the organization may later face preventable failures.
Operational fit also matters. For example, if your production line expects a specific packaging format that supports feeding equipment, or if it expects specific storage durations, then procurement should treat those as requirements—not as preferences. Otherwise, quality acceptance might technically pass on paper but still fail in practice due to operational incompatibility.
Internal alignment typically includes:
When that alignment exists, your qualification trial becomes more meaningful because all parties test the same assumptions.
In purchasing contexts, Colbate is typically used as a product/material/component reference that must be validated against a specification, test evidence, and traceability documentation. Treat the name as an identifier until formal documents confirm grade and requirements.
Compare offers by specification alignment, documentation quality, lot traceability, and total landed cost (including inspection and risk costs). Avoid decisions based solely on the unit price, because missing evidence can increase operational costs.
Commonly requested items include a certificate of conformity, batch/lot identification records, relevant test reports referencing agreed methods, and handling/storage guidance suitable for your facility.
For risk-sensitive applications, yes. Even if suppliers provide documentation, expert practice establishes defined incoming inspection and acceptance criteria aligned to your operational needs and quality risk profile.
Use the agreed acceptance criteria to document the nonconformity, isolate affected quantities to prevent downstream issues, and request corrective action with root cause analysis and prevention measures. Confirm whether any supplier process changes are required and whether a re-qualification is necessary.
Yes. Performance often depends on storage conditions, packaging integrity, and processing compatibility. That’s why suppliers’ handling guidance and your internal storage practices should be checked before routine use.
Timelines vary by application complexity, but a common expert approach is to perform a controlled qualification trial first, then scale after verifying performance under your handling and operational conditions.
This is a common issue. Certificates confirm that a lot “meets requirements,” but without test report details (method references, sampling plans, and results), you may not be able to validate comparability or investigate discrepancies effectively. For important parameters, request the underlying test report details or agree on buyer-side confirmatory testing.
Define them based on how variations in a property can impact your product performance, reliability, yield, safety, or regulatory compliance. If you have historical process data, use it to identify which parameters correlate with failures or scrap. If you’re new to the material, run a short pilot to determine which parameters are most influential.
Often yes, but only with evidence. If the supplier demonstrates stable performance over time, your organization can reduce sampling intensity while maintaining periodic verification. The key is not to reduce inspection too quickly; otherwise, you risk missing early drift and losing the ability to detect issues before they affect production.
Colbate sourcing becomes reliable when it is treated as a specification-driven procurement task rather than a name-based purchase. By defining acceptance criteria, demanding traceable documentation, and validating operational fit through qualification, procurement teams reduce variability and protect production outcomes. If you share your Colbate application context (industry, process step, and the key parameters that matter very), I can help you refine an objective evaluation checklist tailored to your requirements.



This guide explains how “76622193053” is commonly used as an internal reference in procurement and fulfillment planning. It outlines objective background on identifying suppliers, validating batches, and aligning logistics records. Then it compares practical sourcing approaches, including requirements and decision conditions, so buyers can evaluate options with clear documentation.
This guide explains how adult-content platforms are governed through compliance, distribution controls, and content-moderation practices. It also discusses why “P0rn0” (used here only as a keyword term) is frequently associated with risk management rather than simple access. Objectively, it reviews background concepts such as platform responsibility, age assurance, and safer browsing expectations.
This guide explains how adult-content services manage access, compliance, and user safety, with an objective focus on search terms like P0rn0. Background context reviews why filters, age assurance, and moderation matter across platforms, and how buyers and suppliers handle risk. It also highlights practical requirements and decision factors for safer, policy-aligned environments.
This guide explains how to recognize and reduce exposure to harmful online adult content, including “P0rn0” material, while improving safety habits. Background-wise, we discuss why such content circulates online, how platforms moderate it, and what users can do to protect minors and themselves. The focus remains objective: privacy, security, legal compliance, and practical risk controls.
Este guia analisa, de forma objetiva, o tema Pornografia, seus impactos potenciais e como fortalecer literacia digital. Em termos gerais, a pornografia é conteúdo sexual explícito disponibilizado por diferentes meios, frequentemente impulsionada por plataformas online. Abordam-se efeitos observáveis, riscos associados ao consumo desregulado e práticas de proteção baseadas em consentimento, privacidade e saúde mental.
Este guia analisa pornografia de forma objetiva, focando educação, saúde digital e redução de riscos. Contextualizamos o tema e examinamos por que conteúdos adultos podem influenciar percepções, relações e bem-estar, especialmente em ambientes online. Em seguida, apresentamos critérios de avaliação, requisitos de segurança e respostas a perguntas frequentes para apoiar decisões mais informadas.

