This guide explains Colbate in practical, industry-focused terms—covering what it is, how it’s sourced, typical quality considerations, and how buyers evaluate suppliers. It also outlines procurement conditions, documentation checks, and common FAQs. Background context is provided objectively to help professionals compare options without relying on marketing claims.
Colbate is discussed in many procurement conversations as a category name used to describe a specific industrial material or product form—often tied to metalworking, surface treatment, or performance-driven manufacturing workflows. For buyers, the very important starting point is not marketing language, but repeatable outcomes: consistent composition, predictable behavior under processing, traceable supply, and compatibility with downstream steps.
In practical terms, evaluating Colbate means asking: What exact formulation or grade is required? Which standards apply? How is the material packaged and handled during shipping? And—critically—does the supplier provide documentation that matches your internal specifications?
Procurement teams that treat “Colbate” like a technical requirement rather than a generic commodity tend to outperform. They catch variability early, build reliable supplier expectations, and reduce costly production interruptions. That is especially important when Colbate feeds into tightly controlled processes—such as those where small chemistry or particle-size variations can change coating adhesion, corrosion resistance, bonding strength, lubrication performance, or machining outcomes.
Because “Colbate” can function as a shorthand label, buyers should ensure there is an unambiguous bridge from the commercial name to the engineering specification. The bridge includes measurable properties, limits for impurities, traceability requirements, and verified documentation. Without that bridge, purchasing becomes a guess, and quality becomes an expensive afterthought.
Across industrial supply chains, names like “Colbate” often function as shorthand for a family of materials or a specific commercial configuration. In procurement, that shorthand can be helpful—yet it can also obscure critical differences between suppliers, batches, and processing routes. That is why experienced teams treat “Colbate” as a starting label, then immediately translate it into technical requirements.
From an expert perspective, buyers usually succeed when they separate three layers:
In real sourcing situations, the hardest part is not choosing suppliers; it’s converting “what the vendor calls it” into “what your process needs.” A disciplined procurement flow can make the difference between a stable supply relationship and recurring deviations.
It also helps to understand why these mismatches occur. Suppliers may use similar product branding across different manufacturing recipes, or they may update compositions over time due to feedstock availability, regulatory shifts, or process improvements. Meanwhile, buyers may have internal specs written for a certain historical formulation. If the buyer doesn’t force explicit mapping from the product name to the controlling properties, the supply chain can drift without anyone noticing until production quality drops.
Additionally, some “Colbate” references may overlap with adjacent industrial categories. For example, buyers might encounter naming overlap where one supplier’s “Colbate” emphasizes corrosion inhibition while another supplier’s “Colbate” emphasizes machinability. If you don’t demand the controlling metrics, you could accidentally source a product that looks identical on paper but behaves differently in application.
If you are comparing suppliers for Colbate, prioritize measurable criteria over broad claims. The goal is to ensure your team can verify that the received material matches what it was supposed to be.
Below are the very commonly decisive evaluation factors in professional purchasing and quality engineering:
Confirm what your vendor means by “Colbate.” Ask for the precise grade (or equivalent internal code), and request a technical data sheet that you can map directly to your engineering spec. Where possible, insist on batch-level traceability identifiers.
A practical way to enforce clarity is to require the supplier to provide: (a) the grade name exactly as used in their manufacturing system, (b) the specification reference number used internally, and (c) the measured values for key properties (not just ranges) for each batch when you order. If you only get ranges, then incoming inspection becomes more complicated and your acceptance risk increases.
Buyers should also verify the form factor. “Colbate” might be supplied as a powder, pellet, liquid formulation, pre-mixed component, or surface treatment input depending on the industrial context. The physical form can dramatically affect mixing time, deposition behavior, dosing accuracy, and contamination risk. If your production line expects a specific form, treat it as a hard requirement—not a preference.
Finally, consider whether your internal process needs special characteristics that aren’t always part of generic grade definitions. For example, you may need narrow viscosity tolerance, controlled moisture content, specific particle morphology, or defined density. If your process is sensitive, explicitly request those properties as part of the procurement spec.
A credible supplier should provide documentation that aligns with recognized standards used in industrial procurement. For example, compliance reports, material test certificates, and evidence of controlled manufacturing processes are typical expectations. When your downstream process demands strict consistency, request results that match your required acceptance thresholds.
Documentation should not be a pile of generic papers. It should be interpretable and relevant to your acceptance criteria. Buyers can reduce frustration by defining in the RFQ exactly what documents you need and how they relate to your tests. Common examples include:
In some cases, buyers also request third-party test references or audit reports. The goal is not bureaucracy; the goal is confidence. If you have frequent production stops, unexplained variability, or high scrap costs, investing in stronger documentation requirements often pays for itself.
Even when composition is correct, logistics can affect performance. Packaging quality (moisture protection, contamination prevention, labeling integrity) matters. Handling conditions during transport—temperature swings, vibration, and exposure—should be addressed in supplier instructions.
Packaging impacts Colbate performance when the material is sensitive to moisture, contamination, settling, oxidation, volatilization, or degradation. Even if the supplier’s product meets grade at shipment, poor packaging or extended transit can change effective properties upon receipt.
Therefore, buyers should request and verify:
In addition, define the receiving workflow. Procurement should coordinate with warehouse and quality teams so that receipt, inspection, storage, and staging are performed under the same controlled assumptions used by the spec. Many quality problems are not chemical— they are operational. The supplier can’t fix what happens after delivery, but the buyer can reduce variability with clear internal receiving procedures.
Experienced buyers design a practical incoming inspection plan: sampling frequency, test methods, acceptance criteria, and escalation steps. This reduces production surprises and speeds up supplier alignment if early deviations occur.
An effective acceptance strategy balances three competing realities:
Buyers often solve this by structuring acceptance testing in layers. For example:
It is also useful to define “release on results” versus “release to production.” Some organizations hold all lots until test results complete; others allow conditional release while testing. The right approach depends on criticality, process tolerance, and the cost of delaying production.
Escalation should be defined up front. Buyers should specify what happens if incoming tests fail: retest process, stop-ship conditions, containment action, supplier notification timelines, root-cause expectations, and corrective action requirements.
Look beyond price. A supplier’s ability to respond quickly to technical questions, provide documentation on time, and support corrective actions is a core indicator of good reliability.
In many procurement failures, the product wasn’t only wrong; it was wrong repeatedly, and the supplier response was slow. A supplier that can’t explain deviations or fails to provide timely corrective action documentation increases buyer workload and operational risk.
To evaluate supplier capability, buyers can look at:
Supplier responsiveness is especially critical when “Colbate” needs to perform under tight production conditions. When production time is expensive, any supplier that drags on in the early qualification phase becomes a long-term cost center.
Price for Colbate typically varies based on grade, purity or composition requirements, supply volume, and documentation depth (for example, the extent of testing certificates and batch traceability). Because pricing can be sensitive to market conditions and product configuration, buyers should avoid relying on a single number.
Instead, treat cost as a total procurement equation:
To keep procurement decisions objective, teams often calculate a “delivered quality cost,” where the chosen option is the one that minimizes the combined expected cost of purchase plus verification and production risk.
Delivered quality cost is particularly important for materials that are hard to substitute mid-process. For example, if your line is configured around a certain Colbate performance characteristic, nonconforming material can cause yield loss. Even if the unit price is lower, total cost may increase due to scrap, rework, slowed throughput, or customer delivery delays.
Another practical approach is to compare suppliers using a “cost-per-acceptable-batch” mindset. That means factoring the probability that a batch will pass your acceptance criteria on the first attempt. Suppliers with stronger documentation and proven consistency typically reduce your expected retest and rework costs.
Finally, consider contract terms and quality obligations. Price can be “cheap” but your total cost can become expensive if the supplier is vague about replacements, returns, or credit for nonconforming product. For Colbate, where performance sensitivity can be high, contract terms should explicitly define nonconformance handling: timelines, disposition options, responsibility for testing, and how disputes are resolved.
When evaluating suppliers for Colbate, the very effective method is to standardize your request-for-quote (RFQ) so that every vendor responds to the same technical questions. This prevents apples-to-oranges comparisons.
In professional procurement practice, you typically ask for:
Then, you score responses using a weighted model that includes quality evidence and responsiveness, not just sticker price.
To make scoring truly reliable, ensure that quality engineering and procurement jointly define the scoring rubric. For instance, “documentation completeness” could be worth more than “slightly lower unit price,” especially when your process sensitivity is high. Buyers can also include criteria such as:
This also helps with internal alignment. When everyone sees the same scoring model, it reduces disputes later. Quality engineering can trust procurement decisions because the technical requirements were embedded into the RFQ and scored consistently. Procurement can trust engineering because the scoring weights reflect real operational risk.
The prompt requires replacing any city or country mention inside keywords with “nearby.” Since your provided keywords contain no explicit city or country terms, this guide keeps the sourcing logic general and applicable across regions. In practice, buyers often tailor logistics expectations to local infrastructure—port handling practices, warehouse climate control norms, and typical lead-time patterns—while keeping core quality verification steps consistent.
Localization still matters because transit profiles can influence storage conditions upon arrival. For example, the typical temperature and humidity range experienced during shipping can differ based on route length, carrier handling practices, and local warehouse climate control. Buyers can incorporate these differences by requiring suppliers to state shipping conditions and shelf-life constraints, then aligning receiving processes to those stated requirements.
The following supplement is designed as a usable checklist you can hand to procurement, quality, and engineering teams.
| Step | Action | Conditions / Requirements | Output to Confirm |
|---|---|---|---|
| 1 | Translate “Colbate” into a technical specification | Define grade, required properties, and any impurity limits your process tolerates | Written spec section to attach to RFQ |
| 2 | Request documentation packages | Require technical data sheet and example batch test certificates | Vendor packet for verification |
| 3 | Run supplier qualification (paper + sample) | Confirm traceability capability; test incoming samples against acceptance criteria | Qualification result and test records |
| 4 | Define acceptance testing for production lots | Agree on sampling frequency, methods, and escalation triggers | Incoming inspection SOP |
| 5 | Lock logistics and handling conditions | Specify packaging requirements and storage conditions upon receipt | Shipping/handling requirements in purchase order |
| 6 | Place orders with controlled ramp-up | Start with limited quantities; validate performance and process stability | Stable process confirmation |
| 7 | Maintain ongoing supplier performance reviews | Track nonconformance rates, documentation timeliness, and corrective action closure time | Supplier scorecard and improvement plan |
To make this checklist even more actionable, it helps to define “what success looks like” at each step. Step 1 success might mean an engineering sign-off on the specification mapping and a procurement sign-off that the RFQ will request exactly those properties. Step 3 success might mean sample lots meet acceptance thresholds with no unresolved documentation gaps. Step 4 success might mean test methods and sampling plans are written clearly enough that the same outcome occurs regardless of which shift performs the inspection. Step 6 success might mean you can run the material through your real production process without yield impact or unexpected parameter drift.
Additionally, define how you will handle partial compliance scenarios. Sometimes a batch passes the key properties but fails a non-critical attribute (for example, labeling formatting, minor trace impurity outside documentation, or packaging condition that still preserves performance). Decide in advance whether you accept with documented deviation or reject outright. This reduces ad-hoc decisions that often cause disputes between procurement and quality.
Lastly, build in supplier communication triggers. For example, if lead times are changing, if the supplier is experiencing supply chain disruption, or if they mention changes in feedstock, you might require enhanced verification for the next shipment. Colbate procurement should include a “reactive quality plan” tied to supplier change signals, not only to random incoming inspection results.
Because “Colbate” can be used as a commercial shorthand, objective background depends on the underlying category—such as industrial metalworking materials, coatings-related inputs, or engineered compositions. For procurement top practices, the very relevant sources are typically:
If you share your exact Colbate grade or intended application, the evaluation criteria can be aligned more precisely to the relevant standards and testing approaches.
In the absence of exact grade details, buyers can still follow a consistent quality procurement philosophy: require definition, require evidence, verify upon receipt, and maintain feedback loops. This is the essence of quality-centric procurement, and it applies whether Colbate is a component, a treatment input, or a process material.
Quality engineering can further refine which standards matter by linking the material’s properties to the failure modes in the production line. For example, if the primary risk is corrosion, then acceptance criteria should include corrosion-relevant properties and methods. If the primary risk is bonding failure, then acceptance criteria should include relevant chemical or physical properties affecting adhesion or cure behavior. This alignment ensures that testing focuses on what truly drives downstream performance.
Even competent teams can encounter problems. The pattern is usually predictable:
A supplier may use “Colbate” as a label while your engineering team needs a precise formulation. The fix is to require translation from label to measured properties (and document examples).
This failure point often surfaces as inconsistency in performance. A first batch might appear “close enough” during trial runs, but subsequent lots may deviate. When buyers don’t enforce the mapping between name and measured properties, the supplier’s internal variability becomes the buyer’s operational problem.
To reduce this risk, buyers can require the supplier to list key controlling parameters and the allowable ranges. Then, add those parameters to the acceptance plan. When acceptance testing focuses on the controlling parameters, the label matters less.
Some vendors deliver paperwork without clear batch traceability or without test results tied to your acceptance thresholds. Buyers should request batch-level evidence that you can interpret directly.
“Usable documentation” has at least four characteristics:
If documentation is missing method information or uses different measurement units, buyers waste time converting data or making uncertain acceptance decisions. In severe cases, the buyer must repeat tests, increasing costs and slowing release.
If inspection is not aligned with your process sensitivity, deviations slip into production. Conversely, if testing takes too long, production queues stall. A balanced plan reduces both scrap and downtime.
There is a common trap where teams either over-test or under-test. Over-testing can create bottlenecks and lead to production delays, which then tempts teams to “release early” before complete results. Under-testing can allow variability to enter production, where it becomes expensive to correct.
One solution is to prioritize the “most sensitive” properties. Buyers can work with engineering to identify properties that correlate most strongly with performance outcomes. Testing those first provides early warning while keeping turnaround time manageable.
Another solution is to implement a structured sampling and retesting plan. If a lot fails a critical parameter, you may choose to reject. If it fails a non-critical parameter, you may retest or accept with documented deviation. Clear logic prevents inconsistent decisions.
Materials can be sensitive to storage conditions, packaging integrity, and time-in-transit. A structured handling statement included in the purchase order prevents assumptions.
This is a major issue because buyers often assume supplier compliance stops at loading the product. In practice, materials can degrade during transit or after arrival if storage conditions aren’t maintained. Buyers can prevent these failures by specifying:
Additionally, receiving personnel should be trained on what to do if packaging is damaged. For example, a torn seal or a compromised drum liner might require quarantine and additional testing. A procurement plan should align with warehouse procedures to ensure consistent response.
Here is a professional method to compare suppliers that stays objective:
This approach prevents “lowest quote wins” decisions that often create hidden costs later.
To further protect objectivity, define how you will treat “equivalency” claims. Some suppliers may assert that their product is equivalent to your requested Colbate grade. Do not accept equivalency based on verbal assurances. Require data that demonstrates matching controlling parameters, supported by sample testing or historical CoA evidence. If equivalency is allowed, it should be allowed through a documented qualification pathway, not through vague claims.
Also pay attention to changes over time. Suppliers that win quotes by providing strong documentation sometimes later reduce the depth of paperwork or change the internal processes. Your procurement framework should include periodic audits or document verification to ensure they remain aligned. If you establish a baseline now, it becomes easier to detect drift later.
Different suppliers may describe similar materials using slightly different terms. When evaluating Colbate, ensure you understand the meaning of:
It is also helpful for procurement teams to understand a few additional related terms that commonly appear in quality discussions:
By using a shared vocabulary across procurement, quality, and engineering, teams reduce the risk of miscommunication. For example, if procurement hears “the material passes grade checks,” but quality tests verify different parameters than those used by the supplier, the buyer can be misled. Clear definitions prevent these misunderstandings.
Colbate is commonly used as a commercial or category label for a specific industrial material configuration. Because the term can vary by supplier and application, you should request the precise grade, formulation, and technical data sheet to confirm it matches your intended use.
In many organizations, the “exact meaning” is not the label itself but the documented set of properties behind the grade. That is why the most productive sourcing conversations begin with “What are the controlling parameters?” rather than “Who sells Colbate?”
Compare total delivered procurement cost, not only the unit price. Include documentation depth, packaging, shipping, lead time, incoming testing needs, and the risk of process variation that can drive rework or scrap.
When you compare total cost, ensure you use consistent assumptions for test effort and release timing. If Supplier A provides certificates early and Supplier B provides them after the lot is consumed, Supplier B may indirectly increase operational cost even if the unit price is lower. Pricing comparisons should reflect your actual process reality.
At minimum, expect a technical data sheet and batch-level documentation demonstrating traceability. For quality-critical applications, request test certificates that correspond directly to your acceptance criteria and grade definition.
It is also valuable to require that documentation includes: units, test methods, batch identifiers, manufacturing dates, and any applicable shelf-life information. If a supplier’s documents omit method information, your quality team may still be able to interpret results, but interpretive uncertainty increases and may force additional testing.
For new suppliers, sensitive processes, or tight performance tolerances, samples are strongly recommended. A controlled sample verification phase helps confirm compatibility with downstream steps and reduces production disruption.
Even if the supplier claims they are “already qualified” elsewhere, your process conditions may be different. Sample verification tests your specific assumptions about compatibility. This step is especially important when the cost of rework is high or when scrap disposal has constraints.
Implement an incoming inspection plan with clear sampling and acceptance thresholds. Specify handling and storage conditions in the purchase order, require traceability documentation, and define escalation steps for deviations.
Additionally, create a supplier feedback loop. Track nonconformance trends and link them to batch identifiers. If you identify a recurring issue—such as impurity drift, moisture increase, labeling errors, or documentation delay—then require targeted corrective actions from the supplier rather than generalized “improvements.”
Ask the supplier for recommended storage and handling conditions appropriate to the specific Colbate grade. These requirements should be written and aligned with your warehouse capabilities to avoid performance drift.
Make sure your receiving team can enforce the storage requirements. If storage conditions require controlled humidity, ensure the warehouse has the capability. Otherwise, the supplier’s recommended conditions are just paperwork rather than a real quality lever.
They may, but equivalence cannot be assumed. Even if the label matches, composition constraints and process-relevant properties may differ. Confirm equivalence using technical data and, where needed, sample testing.
Consider building a formal equivalency qualification: a documented comparison of key properties plus sample trials in your downstream process. This reduces variability and avoids repeated “near matches” that cause production instability.
Qualification time depends on your sampling plan and testing turnaround. Many teams run a short paper qualification first (documentation review), then follow with sample verification before approving a supplier for routine ordering.
Qualification timelines vary, but a disciplined approach—paper review first, then sample testing—can reduce waste. It prevents you from ordering large volumes before confirming that the supplier’s grade definition and batch traceability meet your acceptance needs.
Colbate procurement is very effective when approached as a specification-and-proof exercise rather than a label-and-hope exercise. By translating the term into concrete grade requirements, demanding traceable documentation, designing a practical incoming inspection plan, and comparing suppliers using normalized total cost and reliability signals, buyers can reduce risk and improve process consistency.
If you provide the intended application and any target properties (or the grade/format you mean by Colbate), the sourcing checklist and acceptance strategy can be tailored more precisely to your operational constraints.
In the end, “What Colbate means” is less about the word itself and more about the measurable, controlled attributes that allow your manufacturing process to produce predictable outputs. Buyers who enforce that definition early—through clear RFQs, strong documentation requirements, meaningful acceptance testing, and structured supplier qualification—create procurement outcomes that are stable, auditable, and cost-effective over the long term.



This guide explains what Xiva is, how suppliers structure pricing, and what to verify before purchasing. Objectively, Xiva is treated as a product or brand identifier used in sourcing and retail listings. Background sections cover procurement considerations, quality checks, and documentation standards, helping buyers compare offers without relying on marketing claims.
This guide explains how 1993-based context can help interpret supply chains, procurement decisions, and supplier reliability in today’s markets. Objectively, “1993” often functions as a reference point in sourcing histories, documentation practices, and product lineage, while supplier-related terms indicate where accountability, traceability, and quality controls are documented across time.
This guide explains how to interpret 1993-era decisions, sourcing choices, and supplier relationships using a disciplined research approach. It then provides objective background on common meanings of “1993” in records, the role of suppliers in quality assurance, and why later due diligence matters for procurement and compliance decisions. No claims are exaggerated; methods emphasize verifiable documentation.
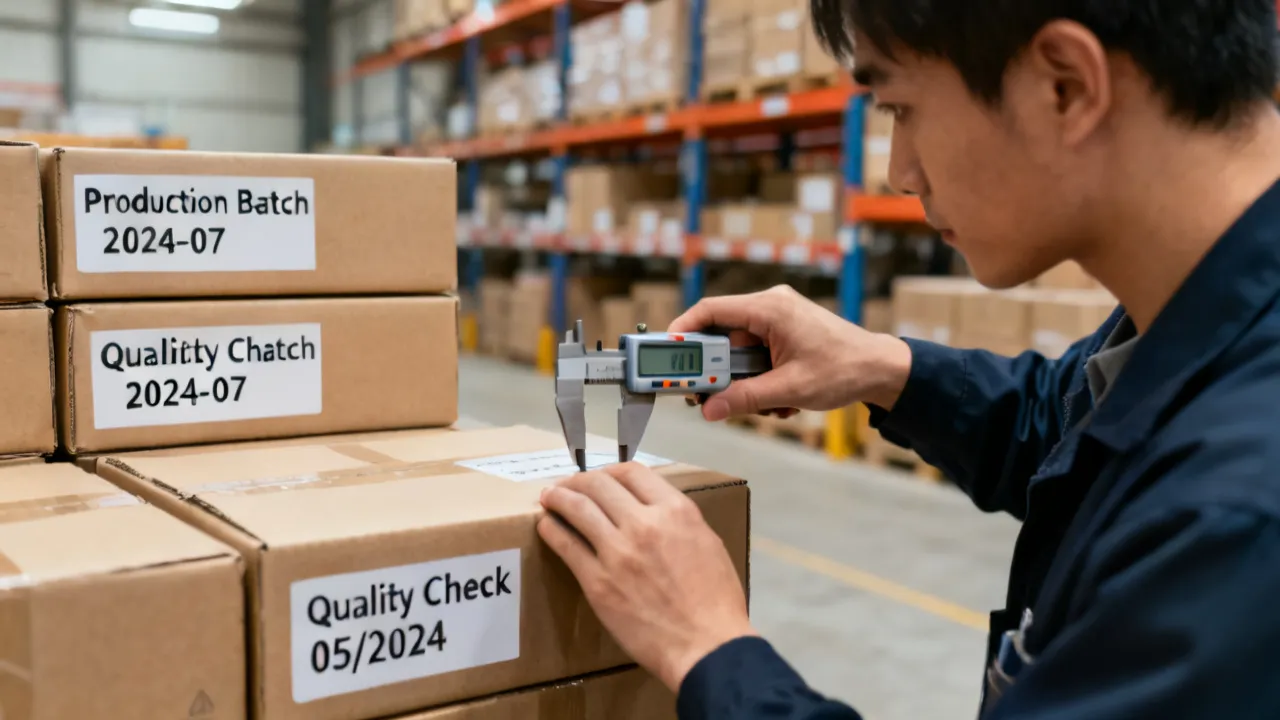
This guide explains how batch or lot identifiers like 16121978 support traceability, quality control, and compliant documentation across suppliers. Objectively, these identifiers connect products to manufacturing records, testing outcomes, and distribution history. We also compare practical requirements for accurate recordkeeping, highlight common risks, and provide expert-led FAQs for procurement and quality teams.
This guide explains how 1993-era product value, supply chain choices, and good vendor relationships shape modern purchasing decisions. It provides objective background on the roles of suppliers, pricing discipline, and documentation practices. It also outlines evaluation conditions readers can apply to assess sourcing risk and maintain quality across time.
This guide explains how the year 1993 continues to influence today’s market expectations and supplier practices. Objectively, 1993 sits in a period of expanding global trade, evolving quality norms, and digitization experiments that shaped procurement thinking. The article connects these themes to practical decision-making, evaluation criteria, and service purchasing habits, helping readers interpret “legacy” without assuming myths.

